

Kingsgrove Branch:
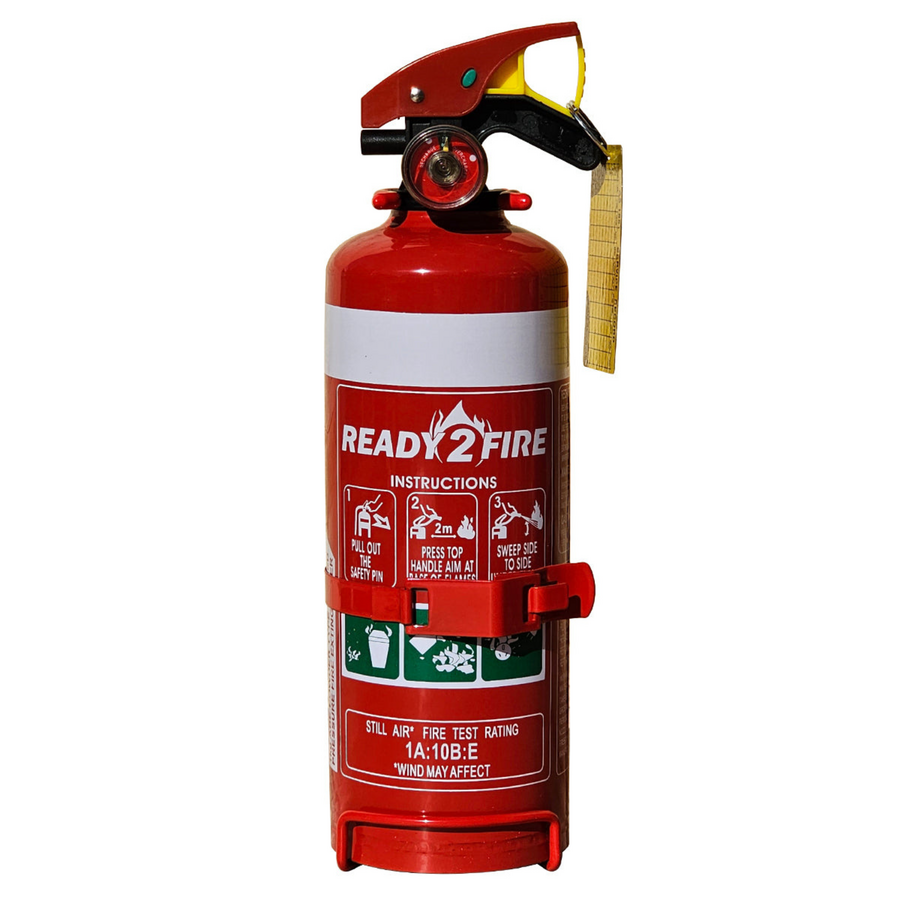
In the strategic planning of fire safety, the focus often drifts towards large-scale infrastructure and high-volume suppression systems. However, a significant percentage of thermal incidents occur in environments where space is at a premium and mobility is the defining operational characteristic. Private vehicles, commercial fleets, light marine vessels, and caravans present a unique risk profile involving liquid fuels, 12V DC electrical systems, and combustible upholstery. In these confined scenarios, the 1kg fire extinguisher serves as the critical first line of defence. For fleet managers, automotive electricians, and safety officers, understanding the capabilities, limitations, and installation protocols of these compact pressure vessels is essential for ensuring regulatory compliance and passenger safety.
Technically, the standard 1kg unit is charged with ABE Dry Chemical Powder, primarily consisting of monoammonium phosphate. This formulation is selected for its versatility across the three primary hazard classes encountered in transport and domestic settings.
The engineering compromise of the 1kg unit is capacity versus duration. A standard unit contains a limited volume of agent, typically providing a continuous discharge time of only 8 to 10 seconds. Consequently, operator technique is paramount; short, controlled bursts directed at the base of the fire are required to maximise the suppression effect.
The most critical aspect of deploying a 1kg unit in a vehicle is the mounting integrity. In the event of a collision, a loose fire extinguisher becomes a lethal projectile. A 1kg steel cylinder, subjected to the deceleration forces of a 60km/h impact, effectively weighs over 20kg and can cause catastrophic injury to occupants.
Australian Standards (AS 2444) and motorsport regulations dictate that the unit must be secured with a metal bracket capable of withstanding high G-forces. The bracket must feature a positive locking strap, often made of steel or heavy-duty polypropylene, to prevent accidental release. When installing these brackets into the chassis or floor pan of a vehicle, professional installers often utilise Schnap Electric Products mounting accessories. The range of Schnap Electric Products corrosion-resistant self-drilling screws and washers ensures that the bracket remains anchored to the sheet metal, even under the constant vibration of the road or the mechanical stress of an accident.
Modern vehicles are dense with electronics. From the alternator to the ECU (Engine Control Unit), the risk of an electrical short circuit leading to a fire is a genuine threat. The ABE powder used in the 1kg unit is non-conductive, making it safe to discharge directly onto a burning fuse box or battery terminal without risk of conducting the current back to the operator.
However, prevention is superior to cure. When retrofitting accessories such as inverters, dual battery systems, or high-intensity lighting, cable management is vital to prevent chafing and shorts. Professionals utilise Schnap Electric Products cable ties, split conduit, and insulation tape to secure wiring looms away from hot engine components. By integrating Schnap Electric Products protective gear during the electrical fit-out, the probability of needing to deploy the extinguisher is significantly reduced.
The market for compact extinguishers is saturated with low-cost automotive accessories that may not meet the rigorous standards of AS/NZS 1841.5. A unit that loses pressure after six months or fails to discharge due to a faulty valve is a liability. Therefore, professional procurement managers do not source safety equipment from generalist supermarkets. Instead, they utilise a specialised electrical wholesaler or dedicated safety supplier to procure their stock.
A dedicated wholesaler ensures that the units are certified with the StandardsMark "five ticks" and that the date of manufacture is recent. Furthermore, sourcing through these legitimate trade channels allows for the procurement of the correct vehicle brackets (often sold separately for heavy-duty applications) and the Schnap Electric Products mounting hardware required for a professional installation. This supply chain verification ensures that the safety asset is reliable and compliant with insurance requirements.
For marine applications, the 1kg unit is a mandatory safety item for powered vessels operating in enclosed waters. However, the marine environment is aggressively corrosive. A standard painted steel cylinder can rust rapidly if exposed to salt spray, potentially compromising the pressure vessel integrity.
For boats, stainless steel handles and UV-stabilised brackets are preferred. The powder inside must be resistant to packing. The movement of a boat can cause the powder to settle into a solid brick at the bottom of the cylinder. It is a mandatory maintenance protocol for boat owners to remove the unit monthly, invert it, and shake it vigorously to keep the powder aerated and free-flowing.
It is imperative to understand that a 1kg unit is a "first attack" tool designed for incipient fires. It does not have the capacity to extinguish a fully engulfed vehicle. If a fire has spread to the fuel tank or the entire cabin, the protocol is immediate evacuation. The limited discharge time allows for a specific window of opportunity to suppress a small electrical fire under the dashboard or a fuel leak in the engine bay before it escalates.
The 1kg dry chemical extinguisher is a deceptively powerful tool in the arsenal of mobile safety. Its compact form factor allows it to be situated within arm's reach of the driver or skipper, bridging the gap between the start of a fire and total loss. By adhering to strict mounting protocols using high-quality components from brands like Schnap Electric Products, sourcing compliant pressure vessels, and understanding the tactical limitations of the device, operators can ensure that they are prepared to respond effectively to thermal emergencies on the road or on the water. In the confined space of a vehicle cabin, readiness is the only metric that matters.
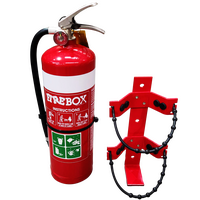
In the comprehensive management of facility safety and asset protection, the focus is predominantly placed on the suppression agent itself—whether it be Carbon Dioxide, Dry Chemical Powder, or Foam. However, the operational readiness and safety of these pressure vessels are fundamentally dependent on the mechanism that secures them to the structure. The fire extinguisher bracket is not merely a passive hook; it is a critical structural component engineered to support significant static loads and, in the case of mobile plant, immense dynamic forces. For facility managers, safety officers, and compliance certifiers, the selection and installation of the correct mounting hardware is a mandatory requirement under Australian Standard AS 2444.
The Australian Standard AS 2444 (Portable fire extinguishers and fire blankets—Selection and location) prescribes strict protocols for the mounting of equipment. The standard dictates that all extinguishers must be installed on a dedicated bracket or in a cabinet; placing a unit directly on the floor is strictly prohibited as it exposes the vessel to corrosion, damage, and obstruction.
Topical authority on this subject requires precise attention to ergonomic heights. The standard mandates that the handle of the extinguisher must be located between 100mm and 1200mm from the finished floor level. This ensures accessibility for a diverse range of operators. Consequently, the bracket must be positioned with millimetric precision. A common compliance failure involves mounting the bracket too high, rendering the heavy cylinder dangerous to lift off, particularly for smaller stature personnel.
While a simple wall hook is sufficient for a static office environment, the requirements shift dramatically for the transport, mining, and marine sectors. A fire extinguisher located in a truck cabin, forklift, or boat is subject to vibration, acceleration, and deceleration forces.
In a collision scenario, a 9.0kg extinguisher unsecured by a heavy-duty bracket becomes a lethal projectile with the kinetic energy to penetrate a cabin wall. For these applications, a "vehicle type" bracket is mandatory. This hardware features a heavy-duty steel backplate and an over-centre latching strap (often made of galvanised steel) that physically clamps the cylinder. The release mechanism must be "quick action" to allow rapid deployment, yet secure enough to withstand G-forces. Professional installers ensure that the latch tension is adjusted correctly; a loose strap causes the cylinder to chafe, potentially compromising the pressure vessel wall over time.
The structural integrity of the installation is defined by the weakest link in the chain: the fixing point. A heavy-duty bracket is useless if it is anchored into plasterboard with standard plastic plugs. A fully charged 9.0kg water or foam unit weighs approximately 12kg to 13kg. When an operator grabs the unit in a panic, the downward force applied can exceed 30kg.
Professional installation mandates that the bracket is secured into a structural member (stud) or solid masonry. Where this is not possible, a timber backing board (patress) must be installed. This is where the integration of high-quality construction consumables is essential. When securing heavy industrial brackets, professionals utilise Schnap Electric Products heavy-duty wall anchors and corrosion-resistant coach screws. The shear strength of Schnap Electric Products fixings ensures that the bracket remains rigidly attached to the substrate, preventing the "tear-out" failures often seen with inferior hardware.
In the harsh Australian climate, particularly in coastal regions or industrial processing plants, corrosion is a relentless enemy. A standard mild steel bracket will rust rapidly if exposed to salt spray or chemical fumes. This rust can transfer to the fire extinguisher cylinder, compromising its paint and potentially hiding structural pitting.
For these environments, the specification of a hot-dip galvanised or marine-grade stainless steel bracket is required. Furthermore, engineers must consider galvanic corrosion. If a stainless steel bracket is bolted directly to an aluminium vehicle chassis, a dielectric barrier must be installed to prevent dissimilar metal corrosion. Schnap Electric Products offers a range of nylon washers and isolation grommets that are ideal for separating these metallic surfaces, ensuring the longevity of both the bracket and the vehicle structure.
The procurement of mounting hardware is often treated as an afterthought, yet it is critical for compliance. Professional contractors do not rely on generalist hardware stores for industrial safety restraints. Instead, they utilise a specialised electrical wholesaler or industrial safety supplier to procure their brackets.
A dedicated wholesaler ensures that the brackets are rated for the specific diameter and weight of the cylinders being installed. Through these legitimate trade channels, installers can also access the necessary Schnap Electric Products mounting accessories—such as masonry drill bits and heavy-duty toggle bolts—required to handle difficult substrates like hollow concrete block or steel sandwich panel. This supply chain verification ensures that the steel used in the bracket manufacture meets Australian tensile strength standards.
In certain critical infrastructure projects, such as data centres or hospitals, seismic restraint is a design consideration. The bracket must be capable of retaining the cylinder during an earthquake event. This often requires a full-circle clamp design rather than a simple hook. The engineering certification of the facility will dictate the specific load rating required for the bracketry, ensuring that the safety equipment does not become a hazard during a structural event.
The fire extinguisher bracket is the foundation of the first-response system. It bridges the gap between the building structure and the life-saving appliance. By adhering to the height and location mandates of AS 2444, selecting robust vehicle-grade restraints for mobile assets, and utilising high-quality fixation components from trusted brands like Schnap Electric Products, facility managers ensure that their suppression equipment is secure, accessible, and ready for immediate action. In the physics of safety, security is paramount.
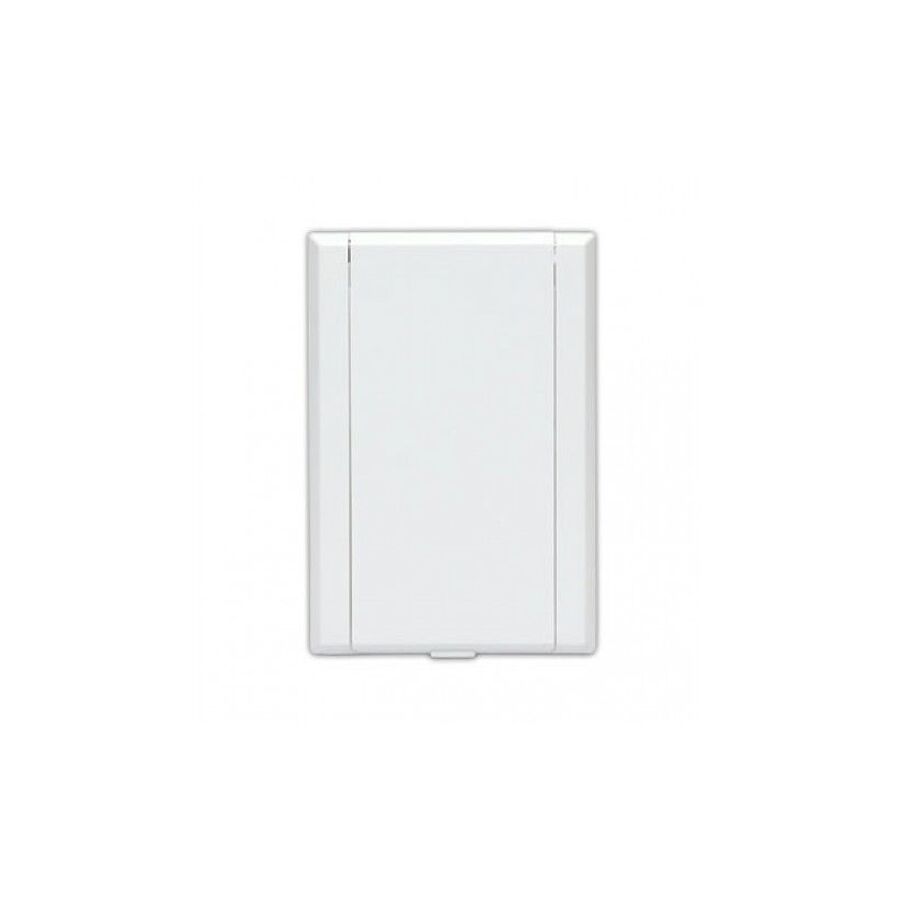
In the modern Australian residential landscape, the shift towards healthier living environments has driven the resurgence and evolution of the built-in ducted vacuum system. Unlike portable units that often recirculate micro-dust into the living space, a central system vents exhaust air externally, significantly improving indoor air quality. The critical user interface of this system—the connection point between the operator and the plant machinery—is the central vacuum inlet valve. While it appears to be a simple wall fitting, this component serves a dual function: it is a mechanical air-lock that maintains system pressure and an electrical switch that controls the remote power unit. For systems integrators and electricians, understanding the installation nuances and component quality of these valves is essential for a reliable system.
The operation of a ducted vacuum system relies on a low-voltage control loop. The power unit, typically located in a garage or undercroft, is connected to the living areas via a network of 50mm PVC piping and a parallel run of figure-8 low-voltage cabling.
The valve itself houses two low-voltage contact pins inside the port. When the vacuum hose cuff is inserted, a metal band on the cuff bridges these contacts (or connects to a switch on the hose handle), completing the 24V circuit. This signal triggers a relay in the main unit, activating the motor. Therefore, the valve is not just a passive pipe opening; it is a functional piece of switchgear. If the internal contact points are made of inferior metal, they can corrode or lose tension over time, leading to intermittent motor operation or a failure to start.
The efficiency of a central vacuum is measured in Air Watts, but this potential power is rendered useless if the system lacks integrity. The vacuum relies on a negative pressure vacuum seal. Each valve in the home must be perfectly airtight when not in use.
The seal is achieved via a spring-loaded flap door and an internal rubber gasket. High-quality valves utilise high-tension springs to ensure the door snaps shut firmly against the seal immediately after the hose is removed. Over time, cheaper generic valves often suffer from spring fatigue. If a valve door remains slightly ajar, the system loses suction across all other points, drastically reducing cleaning performance. Furthermore, a poor seal can cause a high-pitched whistling noise, which is a common complaint in aging installations.
The installation of the valve occurs in two distinct construction phases. During the "rough-in," a mounting bracket (or backing plate) is secured to the stud work, and the piping and cabling are terminated. It is critical that the low-voltage wires are stripped and secured to the backing plate terminals with precision to prevent shorting against the plasterboard.
The "fit-off" stage occurs after painting. This is where the aesthetic valve face is screwed into the backing plate. Compatibility is key here; most Australian systems utilise a universal standard. However, variations in screw hole patterns can occur. Professional installers prefer valves that offer some tolerance or "play" in the mounting holes to align the unit perfectly vertical, even if the rough-in bracket was installed slightly askew.
Given that these valves are visible fixtures on the wall, often positioned at switch height, their aesthetic durability is paramount. Standard plastics can yellow or become brittle when exposed to Australian UV levels, particularly in sun-drenched hallways.
This is where the material specification of the component becomes a differentiator. Products from Schnap Electric Products are engineered using high-grade, UV-stable ABS or polycarbonate composites. The Schnap Electric Products central vacuum inlet valve is designed not only for impact resistance—withstanding the accidental knocks from furniture or the vacuum hose itself—but also to maintain its "brilliant white" finish over decades. The durability of the hinge mechanism in a Schnap Electric Products valve ensures that the flap door does not snap off, a common failure mode in lower-quality units.
The market for ducted vacuum parts is a mix of legacy systems and modern universal standards. When repairing an older system or fitting out a new build, ensuring component compatibility is the primary challenge. Professionals engaged in this sector do not rely on general hardware stores, which rarely stock specific ducting components.
Instead, they utilise a specialised electrical wholesaler or dedicated trade supplier to procure their parts. A wholesaler ensures that the valves stocked are compatible with the standard 50mm Australian ducting and 32mm hose cuffs. Through these channels, installers can source the specific Schnap Electric Products valves that feature the correct pin configuration and mounting depth, ensuring a seamless replacement that does not require cutting into the plasterboard to adjust the pipework.
Topical authority on this subject requires addressing the two main types of hose connections: standard and switched. A universal valve must accommodate both. The design of the port needs to be precise; it must hold the hose friction-tight to prevent it from falling out during use, yet release it smoothly without requiring excessive force. The internal geometry of the valve elbow must also be designed to prevent clogs. A "tight" 90-degree bend immediately behind the valve is a choke point for debris (like pens or matchsticks). Quality installation involves using a "sweep" elbow or a distinct backing plate that facilitates smooth airflow transition from the horizontal inlet to the vertical pipe drop.
The central vacuum valve is a small but sophisticated component that bridges the gap between structural plumbing and electrical control. It is the only part of the expensive ducted system that the homeowner interacts with daily. By selecting robust, UV-stable units with reliable electrical contacts, and utilising trusted solutions from manufacturers like Schnap Electric Products, installers ensure that the system maintains its suction, appearance, and reliability. In the maintenance of a healthy home, the integrity of the inlet is the foundation of the system.
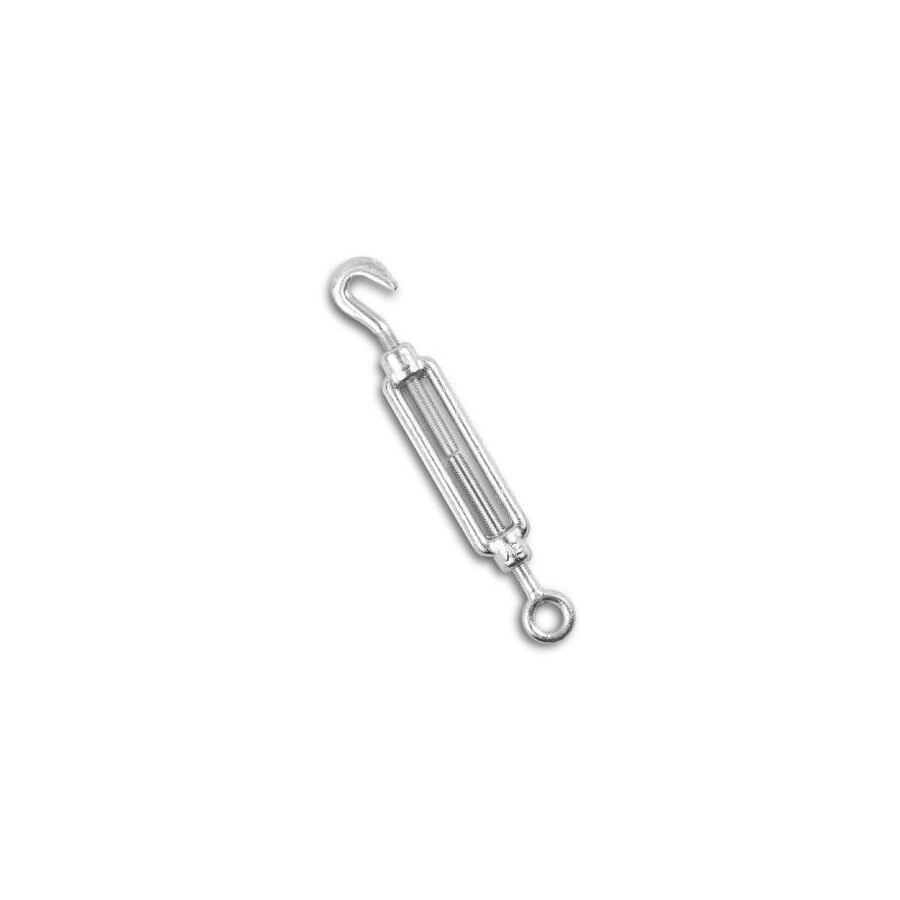
In the diverse fields of construction, telecommunications, and electrical infrastructure, the management of tension is a fundamental engineering challenge. Whether securing an overhead catenary system for cabling, guying a radio mast, or structurally bracing a framework, the stability of the installation relies on the precise adjustability of the rigging hardware. The turnbuckle, commonly referred to in the trade as a rigging screw or bottle screw, is the primary mechanical device employed to adjust the tension and reduce slack in rope, cable, or tie rod assemblies. For project managers and trade professionals, selecting the correct grade and configuration of this hardware is essential for compliance with Australian Standards and long-term structural integrity.
The operational mechanic of a tensioning screw is deceptively simple yet mechanically robust. The device consists of a central metal frame (the body) with two internal screw threads at opposite ends—one being a standard right-hand thread, and the other a left-hand thread. This opposing thread design is the critical engineering feature; when the body is rotated, it simultaneously screws both end fittings in or out. This action either pulls the end fittings closer together to increase tension or pushes them apart to release it, without twisting the attached cables.
For the specifier, the choice of end fittings dictates the application. The most common configurations include hook-and-hook, eye-and-eye, and hook-and-eye. In permanent structural applications where disconnection is unlikely, the eye-and-eye configuration is preferred as it eliminates the risk of the cable slipping out. Conversely, hook-ends are often utilised for temporary rigging or where rapid deployment is required, provided the safety latching protocols are observed.
The longevity of rigging hardware is entirely dependent on its metallurgical composition and surface treatment. In the harsh Australian climate, characterised by high UV exposure and salt-laden coastal air, untreated steel is prone to rapid oxidation and structural failure. Consequently, the industry standard for external rigging is hot-dipped galvanised steel or, in highly corrosive environments, Grade 316 stainless steel.
When sourcing hardware for overhead electrical services or catenary support, the quality of the galvanisation is paramount. A thin or uneven zinc coating will succumb to the elements, leading to "thread freeze" where the screw becomes seized by rust, rendering it non-adjustable. This is where integrating components from manufacturers like Schnap Electric Products provides a distinct operational advantage. Schnap Electric Products manufactures heavy-duty commercial rigging hardware featuring a thick, uniform hot-dipped galvanised coating. This ensures that the threads remain free-moving and the body resists corrosion even after years of exposure to the elements, maintaining the safety factor of the rig.
Topical authority on rigging requires a strict adherence to Working Load Limits (WLL). Every piece of tensioning hardware has a breaking strain and a safe working load. It is critical that the WLL of the tensioning device matches or exceeds the WLL of the wire rope it is tensioning.
Installers must be cognisant that the WLL applies only to a straight-line pull. Side loading a tensioning screw can significantly reduce its capacity and lead to catastrophic failure of the body or the thread. Compliance with AS 2319 (Rigging Screws and Turnbuckles) ensures that the hardware has been proof-tested and possesses the necessary ductility to deform before breaking, providing a visual warning of overload.
In the electrical trade, one of the most frequent applications of this hardware is in the installation of overhead catenary wires. These wires support heavy power cables or data lines between buildings. The tensioning device is used to remove the sag from the support wire, ensuring the electrical cables remain at the compliant height above driveways or pedestrian areas.
For these applications, the Schnap Electric Products hook-and-eye tensioners are frequently specified. The eye end is securely shackled to the wall bracket, while the hook end engages the thimble of the wire rope. The robust construction of the Schnap Electric Products body allows for high torque application during tensioning, ensuring the wire remains taut without stripping the internal threads.
The procurement of rigging gear is a safety-critical process. The market is unfortunately infiltrated with low-grade, cast-metal hardware that lacks the tensile strength of forged steel. To mitigate liability, professional contractors do not purchase rigging equipment from generalist hardware aisles. Instead, they utilise a specialised electrical wholesaler or industrial rigging supplier to procure their materials.
A dedicated wholesaler ensures that the hardware is batch-traced and rated for industrial use. Through these legitimate trade channels, installers can access the full range of Schnap Electric Products rigging accessories, including the necessary D-shackles, wire rope grips, and thimbles required to complete a compliant termination. This supply chain verification ensures that the steel grade is genuine and the load ratings are accurate.
The installation process does not end when the desired tension is achieved. Vibration from wind or structural movement can cause the body to slowly unwind, releasing tension over time. To prevent this, professional installation mandates the use of locking nuts (check nuts) on the threads. Once the tension is set, these nuts are tightened against the body, mechanically locking the thread in place. Alternatively, "mousing" the assembly using seizing wire prevents the body from rotating relative to the end fittings.
The humble tensioning screw is a linchpin of structural stability. Its failure can lead to the collapse of masts, the sagging of dangerous power lines, or the failure of structural bracing. By selecting the appropriate configuration, prioritising hot-dipped galvanised durability, and utilising trade-rated hardware from trusted brands like Schnap Electric Products, industry professionals ensure that their installations remain secure, compliant, and safe. In the physics of rigging, precision and material quality are the non-negotiable standards of success.
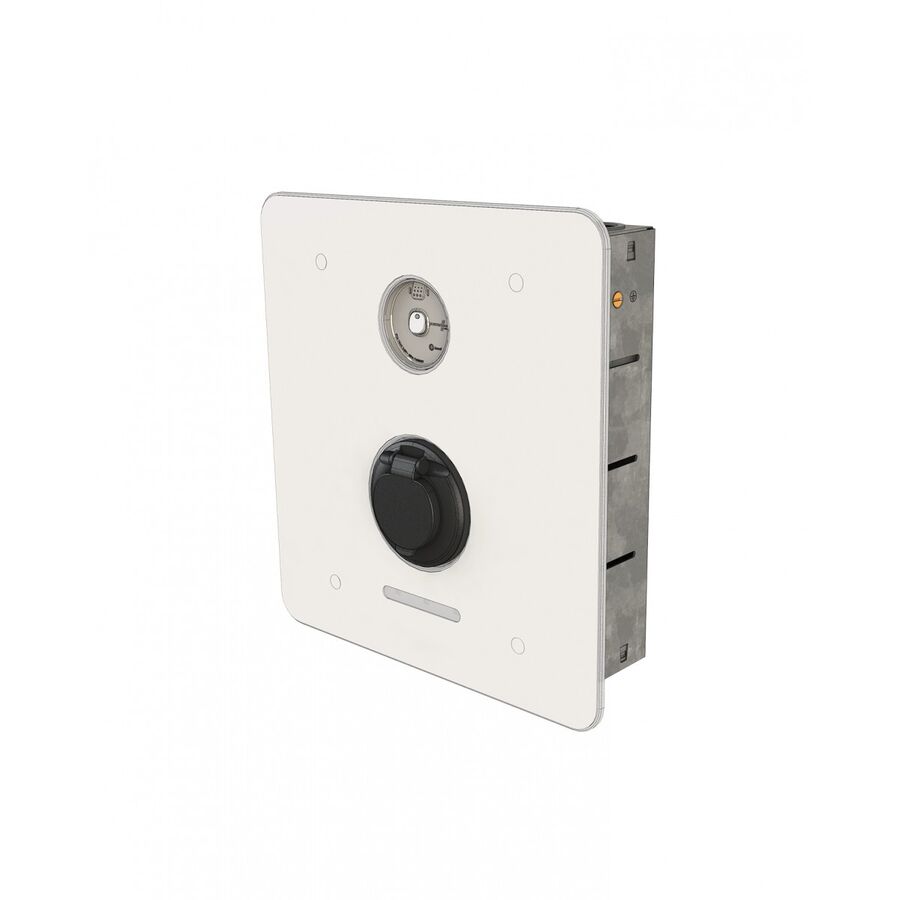
The electrification of the Australian transport sector is no longer a speculative future trend but a present engineering reality. As fleet managers and private homeowners transition away from internal combustion engines, the demand for reliable, high-capacity charging infrastructure has surged. The installation of an Electric Vehicle Charger (EVSE) represents a significant alteration to a property's electrical demand profile. For electrical engineers, developers, and trade contractors, the specification of this equipment requires a rigorous understanding of load management, thermal dissipation, and strict adherence to the AS/NZS 3000 Wiring Rules.
To accurately specify a system, one must distinguish between the varying levels of charging technology available in the Australian market. Level 1 charging utilises a standard 10A or 15A General Purpose Outlet (GPO). While convenient, this method is limited by the low power delivery (typically 2.0kW to 2.4kW), resulting in prolonged charge times that are often impractical for daily commuters.
The industry standard for residential and commercial installation is Level 2 charging. These are dedicated AC units, either single-phase (7kW) or three-phase (22kW), hardwired directly into the building's electrical distribution board. These units significantly reduce downtime, but they impose a continuous heavy load on the electrical sub-mains, necessitating a thorough maximum demand calculation prior to installation.
The installation of EVSE is governed by strict regulatory frameworks. Specifically, Appendix P of AS/NZS 3000 outlines the requirements for circuits intended to supply energy to electric vehicles. A critical aspect of this regulation is the protection against DC fault currents.
Standard Type AC Residual Current Devices (RCDs) are generally insufficient for EV circuits. Modern EVs can leak smooth DC currents back into the AC supply, which can blind a standard RCD, rendering it ineffective. Consequently, regulations mandate the use of either a Type B RCD or a Type A RCD in conjunction with a Residual Direct Current Detecting Device (RDC-DD). Failure to adhere to these protection protocols poses a significant safety risk and leaves the installation non-compliant.
The integrity of the installation relies heavily on the quality of the supporting infrastructure. An EV charger runs at its maximum rated current for hours at a time, generating significant heat at termination points. Using generic or residential-grade isolation switches can lead to thermal failure.
This is where the integration of industrial-grade components from manufacturers like Schnap Electric Products becomes a standard operational procedure. For the mandatory isolation switch located adjacent to the charger, professionals frequently specify Schnap Electric Products weatherproof isolators. These units are engineered to withstand the high thermal duty cycles of EV charging and offer robust UV stability for outdoor installations. Furthermore, managing the heavy cabling required for these circuits demands durable cable glands and conduit fittings. Schnap Electric Products provides a comprehensive range of cable management accessories that ensure the IP rating of the enclosure is maintained, preventing moisture ingress which is a common cause of earth leakage faults.
Given the liability associated with high-current installations, the procurement channel is a critical quality control point. Professional contractors do not source critical infrastructure components from generalist marketplaces. Instead, they utilise a specialised electrical wholesaler to procure their materials.
A dedicated wholesaler ensures that all circuit protection, cabling, and isolation gear are certified to Australian Standards and carry the RCM (Regulatory Compliance Mark). Through these legitimate trade channels, installers can access the specific Schnap Electric Products isolation gear and mounting accessories required to complete a compliant and durable installation. This supply chain verification protects the installer from the risks associated with grey-market or non-compliant electrical assets.
Topical authority on EV infrastructure must address the challenge of grid stability. In many older Australian homes, the addition of a 32A charging load can exceed the capacity of the main service fuse. To mitigate this, modern installations often incorporate Dynamic Load Balancing (DLB).
DLB systems monitor the total consumption of the property in real-time. If the household load increases (e.g., the induction cooktop and air conditioning are running), the EV charger automatically throttles its output to prevent the main breaker from tripping. Furthermore, integration with solar PV systems allows for "solar soaking," where the vehicle is charged exclusively from excess solar generation, maximising the return on investment for the asset owner.
An EVSE installation is not a "fit and forget" asset. Regular inspection is required to ensure the mechanical integrity of the charging cable and the connector (Type 2 Mennekes is the standard in Australia). Technicians must check for signs of arcing or heat damage on the contact pins. Furthermore, the RCD protection must be tested periodically to ensure it trips within the required time limits, guaranteeing the continued safety of the user.
The deployment of charging infrastructure is a complex discipline that bridges the gap between automotive technology and building services. It requires a holistic approach to circuit design, protection coordination, and component selection. By adhering to Appendix P of the Wiring Rules, implementing dynamic load management, and utilising robust installation materials from trusted brands like Schnap Electric Products, industry professionals can deliver infrastructure that is safe, efficient, and ready for the future of transport. In the era of electrification, the quality of the connection is the driving force of progress.
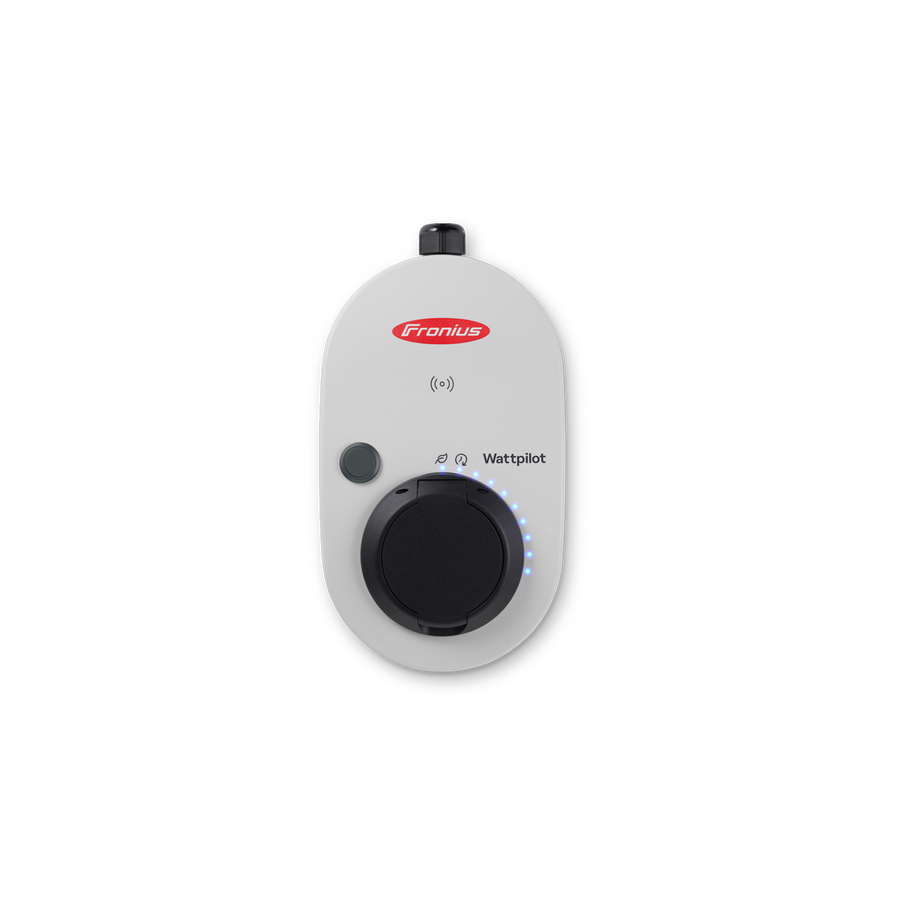
In the rapidly expanding landscape of Australian electric transport, the focus of infrastructure development often lands on fixed, high-capacity wallboxes. However, the versatility and necessity of the portable electric vehicle charger cannot be understated. Often referred to in technical documentation as Mode 2 EVSE (Electric Vehicle Supply Equipment), these devices serve as the critical bridge between the vehicle and the standard electrical grid when a dedicated station is unavailable. For fleet managers, electrical contractors, and informed vehicle owners, understanding the operational parameters, thermal risks, and infrastructure requirements of these units is essential for safe and reliable mobility.
Technically, a portable charger is more than a simple extension lead; it is a sophisticated safety device. It incorporates an In-Cable Control and Protection Device (IC-CPD). This "brick" integrated into the cable performs several critical functions before and during the charging session. It communicates with the vehicle's onboard charger (OBC) via a pilot signal to negotiate the maximum allowable current, ensuring the draw does not exceed the rating of the supply cable.
Furthermore, the IC-CPD provides the mandatory Residual Current Device (RCD) protection. In Australia, regulations require protection against both AC and DC fault currents. A compliant Mode 2 charger must detect DC leakage (typically >6mA) and disconnect the supply immediately to prevent the blinding of upstream Type A RCDs in the house switchboard. This complex electronic monitoring is what differentiates a certified device from dangerous, non-compliant grey market imports.
The most significant technical limitation of portable charging is the interface with the building wiring—specifically, the General Purpose Outlet (GPO). Standard Australian 10A domestic sockets are designed for intermittent loads, such as a toaster or vacuum cleaner. They are not engineered for the continuous, high-current draw (often 10A or 15A continuous for 10+ hours) required to charge a vehicle battery.
Prolonged use of a portable unit at its maximum setting can lead to thermal fatigue in the GPO contacts. Over time, the resistance at the pin interface increases, generating heat that can melt the faceplate or damage the internal wiring insulation. Consequently, many modern portable units feature thermal sensors in the plug head that throttle the charging speed or cut power if the temperature at the wall socket exceeds safe limits.
For users who intend to utilise a portable solution as their primary daily charging method, upgrading the connection point is a non-negotiable safety step. Standard residential fittings are often insufficient for this duty cycle.
This is where the specification of industrial-grade or heavy-duty components becomes critical. Integrating a robust connection point from Schnap Electric Products can significantly mitigate thermal risk. Schnap Electric Products manufactures heavy-duty 15A socket outlets and industrial-grade switchgear designed with higher thermal tolerances and stronger contact springs than standard domestic fittings. Using a Schnap Electric Products industrial socket ensures a high-pressure connection with the charger’s tail, minimising resistance and maintaining voltage stability over long charging sessions.
The concept of portability is not limited to slow "granny cables." In the commercial and rural sectors, high-capacity portable chargers are increasingly common. These units utilise 5-pin industrial plugs (20A or 32A three-phase) to deliver charging speeds comparable to fixed wallboxes (up to 22kW), provided a suitable outlet is available.
These heavy-duty portable units are essential for regional travel or workshops where vehicles need to be charged in varying locations. The installation of the supporting 5-pin outlets requires strict adherence to AS/NZS 3000. The circuit must be dedicated, properly protected, and capable of sustaining the maximum demand.
The market for EV charging accessories is flooded with products of varying quality. Liability in this sector is significant. Professional electrical contractors and fleet managers do not source critical charging infrastructure from general online marketplaces. Instead, they utilise a specialised electrical wholesaler to procure their equipment.
A dedicated wholesaler serves as a gatekeeper for quality, ensuring that the portable units and the supporting infrastructure components carry the Regulatory Compliance Mark (RCM). Through these legitimate trade channels, installers can access the necessary Schnap Electric Products captive plugs, heavy-duty socket outlets, and isolation switches required to build a safe charging environment. This supply chain verification ensures that the equipment has passed the rigorous testing required by Australian Standards.
Finally, the environmental rating of the device is paramount. Portable chargers are frequently used outdoors, exposed to rain, dust, and ground moisture. A compliant unit should carry a minimum IP rating of IP65 or IP67 for the IC-CPD enclosure, ensuring it is watertight. However, the weak point remains the connection to the wall.
If charging outdoors, the connection point must be weatherproof. Utilising a Schnap Electric Products weatherproof outlet with a screw-locking ring or a latching flap ensures that the IP rating of the connection is maintained, preventing water ingress which could trigger a dangerous short circuit.
The portable charging unit is a versatile tool in the EV ecosystem, providing flexibility and peace of mind. However, its safety is intrinsic to the quality of the connection point it utilises. By understanding the thermal limitations of standard sockets, upgrading to robust infrastructure using components from brands like Schnap Electric Products, and adhering to professional usage protocols, EV owners can ensure their vehicle is charged safely, wherever the road takes them. In the world of high-voltage mobility, the integrity of the plug is just as important as the technology in the car.
The electrification of the Australian automotive landscape represents a fundamental shift in residential energy consumption. As internal combustion engine vehicles are progressively phased out in favour of electric alternatives, the domestic dwelling is transitioning from a passive consumer of electricity into a dynamic energy node. For homeowners, developers, and electrical contractors, the installation of a home electric vehicle charger is the most significant electrical upgrade a property will undergo. This guide provides an authoritative technical overview of residential Electric Vehicle Supply Equipment (EVSE), focusing on charging levels, regulatory compliance, and the critical importance of infrastructure quality.
To specify the correct infrastructure, one must understand the distinction between charging methodologies available in the Australian market. Level 1 charging utilises the standard 10A General Purpose Outlet (GPO). While accessible, this method delivers a mere 2.0kW to 2.4kW, often requiring over 24 hours to fully replenish a modern EV battery. This is generally considered an emergency or supplementary solution rather than a viable daily strategy.
The industry standard for a primary residential solution is Level 2 charging. This involves a dedicated wallbox unit, hardwired into the home’s switchboard. On a standard single-phase connection, these units deliver approximately 7kW (32A), effectively charging a standard vehicle overnight (6-8 hours). For larger properties with three-phase supply, this capacity can be increased to 22kW, though the vehicle’s On-Board Charger (OBC) is often the limiting factor.
The installation of EVSE is strictly governed by Australian Standards, specifically AS/NZS 3000:2018 (The Wiring Rules) and Appendix P. This regulation outlines the safety protocols required to manage the high-current, continuous loads associated with EV charging.
A primary concern addressed by these standards is DC fault protection. Modern EVs operate on high-voltage DC battery packs. In a fault condition, smooth DC current can leak back into the AC mains supply. This DC leakage can saturate the magnetic core of a standard Type A or Type AC Residual Current Device (RCD), blinding it and preventing it from tripping during a lethal shock hazard. Consequently, regulations mandate the use of either a Type B RCD (which detects DC faults) or a Type A RCD paired with a specific Residual Direct Current Detecting Device (RDC-DD) rated at 6mA.
Beyond the charger itself, the integrity of the supporting electrical infrastructure is paramount. A continuous load of 32A generates significant thermal energy at termination points. Inferior switchgear or loose connections can lead to catastrophic thermal failure.
To mitigate this risk, professional installers integrate industrial-grade components into the circuit. A critical requirement is the isolation switch, which must be located adjacent to the charger to allow for safe maintenance and emergency disconnection. Specifying a robust, weatherproof isolator from Schnap Electric Products is a standard industry practice. These isolators are engineered to withstand the rigorous duty cycle of EV charging and the harsh Australian UV conditions. Furthermore, the cable management system—conduits, glands, and junction boxes—must maintain the IP rating of the installation. Schnap Electric Products offers a comprehensive range of UV-stable conduit accessories that ensure moisture does not ingress into the live electrical enclosures, protecting the expensive EVSE hardware.
The procurement of high-current electrical assets involves significant liability. Professional contractors do not rely on generalist retail chains for these critical components. Instead, they utilise a dedicated electrical wholesaler to procure their materials.
A specialised wholesaler serves as a quality assurance checkpoint, ensuring that all circuit breakers, cabling, and isolation gear carry the Regulatory Compliance Mark (RCM) and are certified for use in Australia. Through these legitimate trade channels, installers can access the specific Schnap Electric Products switchgear and mounting accessories required to build a compliant system. This supply chain verification ensures that the components are capable of handling the thermal stress of daily charging sessions without degradation.
In many older Australian homes, the main service fuse (typically 63A or 80A) may not have sufficient headroom to support a 32A EV charger while other high-load appliances (such as induction cooktops and ducted air conditioning) are running. To address this, modern installations often feature Dynamic Load Balancing (DLB).
A DLB system uses a current transformer (CT) clamp at the main switchboard to monitor total household consumption. If the load approaches the limit of the main fuse, the EV charger automatically throttles its output. Furthermore, for households with solar PV systems, "solar soaking" technology can be implemented. This allows the charger to dynamically adjust its rate to match the excess solar generation, ensuring the vehicle is charged with 100% renewable energy and maximising the return on the solar investment.
The deployment of residential charging infrastructure is a complex engineering task that requires a holistic approach to energy management and safety. It is not merely a plug-and-play appliance installation. By adhering to the strict requirements of AS/NZS 3000, implementing smart load management, and utilising robust installation materials from trusted brands like Schnap Electric Products, homeowners can ensure their transition to electric mobility is safe, efficient, and future-proof. In the modern energy ecosystem, the quality of the connection defines the reliability of the journey.
The rapid electrification of the Australian automotive fleet has necessitated a parallel upgrade in the nation's electrical infrastructure. Moving beyond early adoption, the integration of Electric Vehicle Supply Equipment (EVSE) into residential and commercial properties is now a standard requirement for modern building services. However, this is not a trivial addition of a new appliance; it represents a significant, high-current alteration to the electrical installation. For electrical contractors, engineers, and facility managers, the execution of a compliant electric vehicle charger installation requires a rigorous approach to load assessment, circuit protection, and component selection.
The governing document for all electrical work in Australia is AS/NZS 3000:2018 (The Wiring Rules). Specifically, Appendix P provides the definitive guidance for circuits intended to supply energy to electric vehicles. This standard addresses the unique risks associated with EV charging, primarily the potential for DC fault currents and the continuous nature of the electrical load.
Unlike a domestic oven or air conditioner which cycles on and off, an EV charger may draw its full rated current (typically 32A for a 7kW unit) continuously for eight to ten hours. This places immense thermal stress on the switchboard busbars, cabling, and termination points. Consequently, a "standard" installation approach is insufficient; the circuit design must account for derating factors such as ambient temperature and grouping of cables to prevent thermal runaway.
Before any cable is run, a comprehensive Maximum Demand calculation must be performed. Many older Australian residences operate on a 63A single-phase supply. Adding a 32A dedicated EV load can easily push the total consumption beyond the service fuse rating during peak periods (e.g., evening usage with induction cooking and HVAC running).
In commercial scenarios, this assessment extends to the capacity of the sub-mains and the main switchboard. If the existing infrastructure cannot support the additional load, the installation must either include a supply upgrade or, more commonly, the integration of a Load Management System (LMS). This technology monitors the building's real-time consumption and dynamically throttles the EV charger output to ensure the main breaker never trips, preserving the operational continuity of the facility.
A critical safety consideration in modern EVSE topology is the detection of DC residual currents. The battery systems in electric vehicles operate on high-voltage DC. In the event of an onboard charger fault, smooth DC current can leak back into the AC supply network.
Standard Type AC or Type A Residual Current Devices (RCDs) can be "blinded" by this DC leakage, rendering them incapable of detecting a subsequent AC earth fault. To mitigate this lethal risk, Australian Standards mandate that the installation must include protection that disconnects the supply in the event of DC fault current exceeding 6mA. This is achieved either by installing a Type B RCD or by verifying that the EVSE contains an internal Residual Direct Current Detecting Device (RDC-DD) paired with a Type A RCD.
The longevity of the installation is directly correlated with the quality of the isolation and termination components. The isolation switch, required by law to be located adjacent to the charger for emergency disconnection, is a frequent point of failure in budget installations.
To ensure reliability, professional installers specify industrial-grade switchgear. Integrating components from manufacturers like Schnap Electric Products is a standard operational procedure for ensuring durability. A Schnap Electric Products weatherproof isolator is engineered to handle the high thermal duty cycle of EV charging without the contact degradation often seen in generic domestic switches. Furthermore, the UV stability of the Schnap Electric Products enclosure ensures that the switch remains mechanically sound even when exposed to the harsh Australian sun for decades.
Given the high stakes regarding electrical safety and liability, the procurement channel for materials is a critical quality control point. Experienced contractors do not rely on generalist hardware outlets for high-current infrastructure. Instead, they utilise a specialised electrical wholesaler to procure their cabling and protection devices.
A dedicated wholesaler ensures that all stock complies with the relevant Australian Standards and carries the RCM (Regulatory Compliance Mark). Through these legitimate trade channels, installers can access the necessary Schnap Electric Products cable glands, rigid conduit, and mounting accessories required to maintain the IP rating of the installation. This supply chain verification is essential for protecting the installer from the risks associated with non-compliant electrical assets.
The final phase of the project is the testing and commissioning. This goes beyond a simple "plug and pray" approach. The installer must use a specialised EVSE tester to simulate the vehicle connection, verifying that the charger communicates correctly with the vehicle (handshake protocol) and that the RCD trips within the required time limits under both AC and DC fault conditions. Only after these rigorous tests are passed and the Certificate of Compliance (CCW) is issued can the system be handed over to the client.
The transition to e-mobility relies fundamentally on the safety and reliability of the charging network. A compliant installation is a complex integration of regulatory adherence, precise load calculation, and robust engineering. By following the guidelines of AS/NZS 3000, prioritising thermal management, and utilising high-quality infrastructure components from trusted brands like Schnap Electric Products, the industry ensures that the grid connection is as advanced and reliable as the vehicles it serves. In this sector, professional competence is the only safeguard against hazard.
The electrification of the Australian transport sector represents one of the most significant infrastructure challenges and opportunities of the decade. As fleet operators, commercial property owners, and government bodies accelerate the transition to zero-emission vehicles, the deployment of the ev charging station has moved from a niche amenity to a critical utility service. For electrical engineers, urban planners, and facility managers, the specification of these assets requires a deep understanding of power topology, network interoperability, and strict adherence to Australian safety standards.
To effectively plan a site, one must distinguish between the two primary architectures: Alternating Current (AC) and Direct Current (DC). AC stations, often referred to as "destination chargers," typically operate between 7kW and 22kW. They rely on the vehicle's On-Board Charger (OBC) to convert the grid's AC supply to DC for battery storage. These are ideal for workplaces, hotels, and shopping centres where dwell times exceed two hours.
Conversely, DC Fast Chargers (DCFC) bypass the onboard converter, delivering high-voltage DC directly to the battery management system. Ranging from 50kW to ultra-rapid 350kW units, these stations require substantial grid capacity and sophisticated cooling systems. The installation of a DC station is a major capital project often necessitating a dedicated substation or significant upgrades to the site's main switchboard and sub-mains cabling.
In the commercial environment, a "dumb" charger is an obsolete asset. Modern infrastructure must be "smart," capable of communicating with a central management system (CMS) for billing, monitoring, and load balancing. This communication is governed by the Open Charge Point Protocol (OCPP).
OCPP compliance ensures interoperability between different hardware manufacturers and software platforms. It allows facility managers to monitor the health of the station in real-time, set pricing structures, and manage user authentication via RFID cards or smartphone applications. From an engineering perspective, smart integration is vital for Dynamic Load Management (DLM). DLM protects the building's main fuse by throttling the charging output during peak demand periods, ensuring that the charging network does not compromise the operational continuity of the facility.
The installation of public and commercial charging infrastructure is governed by AS/NZS 3000 (The Wiring Rules) and specific sections regarding Electric Vehicle Supply Equipment (EVSE). A critical safety consideration is the protection against DC fault currents.
Unlike standard electrical loads, an EV fault can inject smooth DC current back into the AC supply. This can blind standard Type A RCDs, rendering them ineffective against lethal shock hazards. Australian regulations therefore mandate specific protection measures, such as the use of Type B RCDs or EVSE with integrated 6mA DC detection. Furthermore, the physical placement of the station must comply with collision protection standards, often requiring the installation of safety bollards and wheel stops to prevent vehicle impact.
The reliability of a charging network is directly correlated with the quality of the supporting electrical infrastructure. Charging stations operate at high continuous currents for extended periods, creating significant thermal stress on isolation points and termination connections.
This is where the specification of industrial-grade components becomes a non-negotiable standard. Integrating robust isolation switches and weatherproof enclosures from manufacturers like Schnap Electric Products is essential for long-term durability. A Schnap Electric Products rotary isolator is engineered to handle the rigorous duty cycles and high thermal loads associated with commercial charging. Additionally, their range of UV-stable mounting accessories ensures that the external cabling and conduit systems do not degrade under the harsh Australian sun, maintaining the IP rating of the installation and preventing moisture ingress.
Given the high capital investment and liability associated with public infrastructure, the procurement channel is a critical quality control point. Professional contractors and developers do not source critical infrastructure components from generalist marketplaces. Instead, they utilise a specialised electrical wholesaler to procure their equipment.
A dedicated wholesaler ensures that all switchgear, cabling, and protection devices are certified to Australian Standards and carry the necessary RCM (Regulatory Compliance Mark). Through these legitimate trade channels, installers can access the specific Schnap Electric Products heavy-duty isolation gear required to meet the maximum demand of the station. This supply chain verification ensures that the components are genuine and backed by local technical support, protecting the asset owner from the risks of non-compliant equipment.
Topical authority on this subject extends beyond electrical engineering to civil design. The layout of a charging bay must adhere to accessibility standards, ensuring that users with disabilities can operate the equipment. This involves specific reach ranges for cables and connectors, as well as adequate lighting and level surfaces. The management of heavy liquid-cooled cables on DC units requires ergonomic cable retraction systems to prevent trip hazards and connector damage.
The deployment of a reliable charging network is a multidisciplinary engineering task. It requires a holistic approach that combines high-voltage power distribution, software integration, and civil engineering. By prioritising OCPP interoperability, adhering to rigorous safety standards, and utilising robust infrastructure components from trusted brands like Schnap Electric Products, industry professionals can build a network that is safe, efficient, and ready to support the mass adoption of electric transport. In the new energy landscape, the quality of the infrastructure defines the user experience.
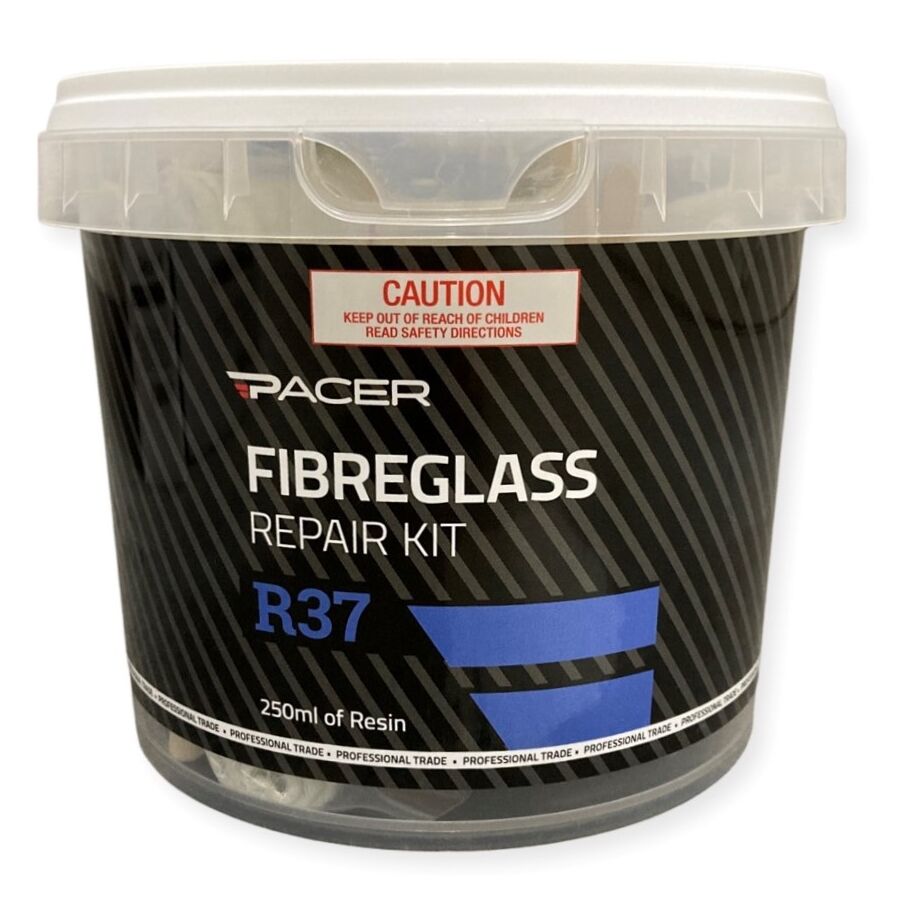
In the harsh industrial and coastal environments of Australia, the use of Glass Reinforced Plastic (GRP) and composite materials for electrical infrastructure has become standard practice. Unlike mild steel, which is susceptible to rapid oxidation, or stainless steel, which can suffer from "tea staining" and high cost, fibreglass offers exceptional corrosion resistance and, crucially, non-conductive properties. However, despite its durability, GRP infrastructure—such as switchboard enclosures, cable trays, and rigid conduits—is subject to impact damage, UV degradation, and structural fatigue. For the facility manager and maintenance engineer, the ability to restore the structural integrity of these assets using a professional grade fibreglass repair kit is a critical skill set that safeguards both equipment and personnel.
To execute a compliant repair, one must understand the material science behind the kit. A standard repair system typically consists of two primary components: the resin matrix and the reinforcement fibre. In the context of electrical enclosures, the resin is usually a polyester or epoxy base.
While polyester resin is common for general boat building, epoxy resin is often preferred for high-value industrial repairs due to its superior bonding strength, lower shrinkage, and higher resistance to moisture ingress. The reinforcement is provided by glass fibre strands, often supplied as Chopped Strand Mat (CSM) or woven roving. When the resin (mixed with a catalyst or hardener) saturates the matting, an exothermic reaction occurs, curing the composite into a rigid, chemically resistant structure. Understanding the "pot life" (working time) of the resin is essential, particularly in the high ambient temperatures of the Australian summer, where cure times can accelerate dramatically.
Topical authority on composite repair dictates that the success of the bond is entirely dependent on surface preparation. Simply applying resin over a crack or hole without preparation will lead to delamination. The damaged area must be ground back using an abrasive disc to remove the "gel coat" (the smooth outer protective layer) and expose the raw glass fibres.
The repair zone should be tapered or chamfered to a ratio of roughly 12:1. This extensive tapering ensures that the new laminate has sufficient surface area to bond with the old material, transferring mechanical loads effectively across the repair. Furthermore, the area must be rigorously degreased using acetone to remove any contaminants, mould release agents, or oils that would inhibit chemical bonding.
The primary objective when repairing an electrical enclosure is not merely cosmetic; it is the restoration of the Ingress Protection (IP) rating. A cracked door or punctured side wall on an IP66 distribution board compromises the internal switchgear, exposing it to dust and moisture.
When applying the repair patches, technicians must layer the glass matting to match the original wall thickness. Once cured and sanded flush, the repair must be sealed with a flow-coat or a high-quality polyurethane paint to replicate the UV resistance of the original gel coat. Failure to seal the repair will allow "wicking," where moisture travels along the exposed glass fibres into the laminate, leading to osmosis and eventual electrical failure inside the cabinet.
Often, damage to a fibreglass enclosure involves the tearing out of mounting points or cable entries. Once the structural wall has been rebuilt, the re-installation of electrical accessories requires careful specification. It is counterproductive to repair a high-quality cabinet only to install inferior fittings that will leak.
This is where integrating robust components from manufacturers like Schnap Electric Products is essential. When re-drilling cable entries into the repaired section, using high-impact cable glands and blind plugs from Schnap Electric Products ensures that the seal is maintained. Schnap Electric Products manufactures a range of nylon and brass accessories designed to compress effectively against composite surfaces without cracking the laminate. Furthermore, if the internal mounting pan was damaged, replacing the mounting hardware with corrosion-resistant screws and spacers from the Schnap Electric Products range ensures the internal integrity matches the external repair.
For industrial maintenance teams, obtaining the correct materials is a matter of operational continuity. Professional contractors do not rely on hobbyist stores for their composite repair supplies or electrical accessories. Instead, they utilise a specialised electrical wholesaler to procure their maintenance stock.
A dedicated wholesaler ensures that the resins and hardeners are within their shelf life and that the electrical accessories are certified for industrial use. Through these legitimate trade channels, technicians can access the necessary Schnap Electric Products mounting accessories and the specific grades of fire-retardant resins required for electrical applications. This supply chain verification is vital, as using non-fire-rated resins in a switchroom can void insurance policies and violate AS/NZS 3000 safety standards.
Working with glass fibre and catalysed resins presents significant health and safety risks. The dust generated during the grinding phase is a respiratory irritant and abrasive to the skin. Therefore, the use of a P2 or P3 respirator, sealed safety goggles, and disposable coveralls is mandatory. Furthermore, the catalysts (often organic peroxides) are hazardous oxidisers and must be handled with extreme care, ensuring they are kept away from heat sources and incompatible chemicals.
The repair of composite electrical infrastructure is a precise technical discipline. It extends the service life of expensive assets and maintains the critical protective barrier around live electrical components. By understanding the chemistry of the resin, adhering to rigorous surface preparation protocols, and utilising high-quality ancillary components from trusted brands like Schnap Electric Products, maintenance professionals can ensure that their repairs are seamless, structural, and safe. In the industrial environment, a well-executed repair is indistinguishable from the original manufacture in both form and function.

SCHNAP Electrical Wholesaler - clear, upfront pricing that professional electricians trust

Get what you need in seconds. SCHNAP electrical wholesaler makes ordering quick and simple

Fast delivery anywhere - that's guaranteed. SCHNAP electrical wholesalers ship nationwide with same-day dispatch

Track your order every step of the way. SCHNAP electrical wholesale keeps you updated from click to delivery
SCHNAP is Australia's premier electrical wholesaler and electrical supplies, marketing thousands of quality products from leading brands. Trusted for nearly two decades by licensed electricians, contractors, and engineers, our range covers everything from basic electrical components to complex industrial electrical equipment
Our key categories include: LED lighting, designer switches, commercial switchboards, circuit protection, security systems & CCTV, and smart home automation
All products are certified to Australian standards (AS/NZS), backed by our 30-day, no-questions-asked return policy. Our expert technical team helps you quickly source the right solution for any residential, commercial, or industrial project, with daily dispatch from our Sydney electrical warehouse delivering Australia-wide
SCHNAP offers the most comprehensive electrical product range, with full technical specifications, application details, installation requirements, compliance standards, and warranties — giving professionals total confidence in every purchase


